
Send Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
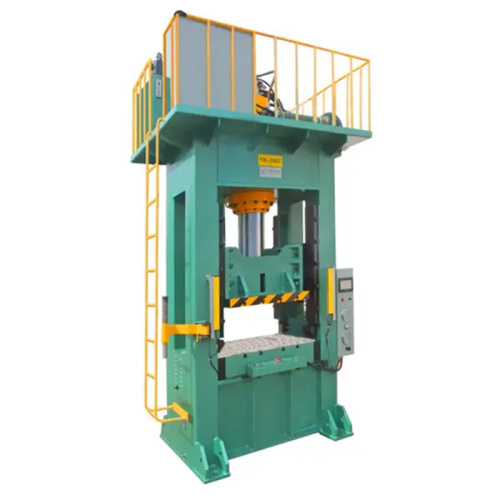
The 50T Powder Press is engineered for powerful, precise compaction, helping manufacturers achieve material densities of up to 99% while significantly reducing powder loss. Its controlled forming process supports consistent part quality, efficient material usage, and lower production costs, making it a practical solution for demanding powder-forming applications. While “zero waste” may be an ambitious goal, this press is designed to minimize waste and maximize productivity without compromising precision or performance.


A 50-ton powder press can apply up to about 500 kN of pressing force, but force alone does not guarantee 99% density or zero waste.
When I evaluate a powder press, I look at the powder, part shape, die size, compaction pressure, lubrication, ejection method, and density test method. These details decide the result. The machine rating is only one part of the process.
A claim of “99% density” needs a clear reference. It may mean 99% of the material’s theoretical density, 99% of a target density, or 99% uniformity across the part. These are different measurements.
A 50T press normally refers to its maximum nominal pressing force. The actual pressure on the powder depends on the projected area of the compact.
For example, a 50-ton force applied to a part with a pressing area of 314 mm² creates a much higher pressure than the same force applied to a part with an area of 1,000 mm².
The basic relationship is:
Compaction pressure = Pressing force ÷ Pressed area
A small iron powder component may receive enough pressure to reach a high green density. A larger part made from the same powder may need a larger press, a different tool design, or multiple pressing stages.
I would not select a press by tonnage alone. I would calculate the required pressure from the part’s geometry and powder data.
The answer depends on the material and the production method.
Some metal powders can reach high green density under strong compaction. Spherical powders, narrow particle-size distributions, good flow, controlled lubrication, and suitable die filling can help reduce empty spaces between particles.
Traditional single-action pressing may still leave pores inside the compact. These pores can remain after sintering. A part may look solid from the outside while its internal density varies from one area to another.
A 99% theoretical density target may be possible for certain materials and shapes after extra processing, such as:
These methods raise equipment cost and process complexity. They also change the meaning of “zero waste.”
For a simple iron powder bushing, a properly designed die may produce a dense and consistent compact. A thin-walled part, a tall part, or a shape with deep steps can show density differences because the powder does not move evenly during pressing.
Powder pressing can reduce material waste compared with machining a part from a solid billet. It does not usually create zero waste.
Common material losses include:
Some unused powder may be collected and reused. That practice depends on the material, contamination control, particle-size change, and internal quality rules. Powder from different batches should not be mixed without a clear control method.
I prefer to describe the process as low-waste powder compaction rather than zero-waste production. That wording gives buyers a more useful expectation.
Imagine that I need to compact a cylindrical iron powder part with a diameter of 20 mm.
The projected area is about 314 mm². A 50T press provides approximately 500,000 N of force. The theoretical pressure would be close to 1,590 MPa if the full force acted across that area.
The actual pressure may differ because of:
The lower section of a tall compact may receive less effective pressure than the area near the punch. This can lead to density variation and cracks during ejection.
The calculation shows that a 50T machine may suit some small components. It does not prove that every 20 mm part will reach 99% density.
I would ask the equipment supplier for process data rather than relying on a short marketing statement.
The test should include:
Powder type and grade
Iron, copper, ceramic, graphite, and other powders behave differently.
Part drawing
Diameter, height, wall thickness, holes, steps, and tolerances affect filling and pressure.
Pressing force and pressure
The supplier should show how the pressure was calculated.
Green density
This is the density after pressing but before sintering.
Sintered density
This value may differ from green density because the part can shrink or develop defects.
Density test method
Archimedes testing is often used for porous metal parts, but the test setup and sample preparation need control.
Waste calculation
The supplier should define whether waste includes feeder residue, rejected parts, dust, and unused powder.
Production sample size
One successful sample does not represent stable production. I would review results from multiple batches.
A good trial should record powder weight, fill height, pressing force, ejection force, green density, sintered density, dimensions, and rejection rate. This data tells me more than the machine label.
Tool design has a major effect. A floating die, double-action pressing, or multiple punches can improve pressure distribution. Proper die lubrication can reduce wall friction and lower the risk of cracks.
Powder preparation also matters. Poor flow can create uneven filling. Excessive lubricant may reduce compact strength or leave unwanted residue during sintering. Moisture and contamination can change the pressing behavior.
The operator’s settings need control as well. Feed speed, fill depth, dwell time, punch movement, and ejection speed can all affect the finished part.
A 50T powder press can be a useful choice for small and medium powder components when the tool and powder are matched correctly. It may support low material loss, but it should not be treated as a guarantee of 99% density or zero waste.
My view is simple: ask for a density definition, a part-specific pressure calculation, test records, and a complete material balance. When a supplier provides those details, I can judge the machine on measurable performance rather than a broad claim.

A powder press can look simple from the outside: fill the die, apply force, release the part. In production, the result depends on much more than press tonnage. Powder flow, fill depth, tooling design, lubrication, compaction speed, and sintering conditions all affect density and scrap.
A 50T powder press gives me a useful working range for small and medium powder-metal parts. It can support repeatable forming when the tool area, powder type, and target density are matched to the machine. The goal is not to promise zero waste or 99% density for every material. The goal is to build a process that moves close to those targets without creating unnecessary powder loss.
Density should be defined before selecting a press.
A compact may reach a high green density directly after pressing, then change during debinding or sintering. Some powders shrink. Others expand slightly. The final density depends on the material and the thermal cycle.
When I discuss 99% density, I first ask:
For a simple cylindrical component, a 50T press may produce stable results with a well-designed die. A deep part with several height levels may show density differences even when the press reaches the planned load.
The press does not remove waste by itself. Waste reduction comes from controlling the full forming cycle.
I normally review these points:
1. Match force to projected area
A 50T press can deliver up to about 50 metric tons of pressing force, depending on the machine design and operating conditions. The usable pressure at the powder bed depends on the compact area.
A small part may receive enough pressure for strong compaction. A large part may need a lower target pressure, a different tool layout, or another press size. Calculating the required force before making the die helps prevent weak parts and tool overload.
2. Improve powder filling
Uneven filling creates density variation. A part can look acceptable on the outside while showing cracks, weak edges, or different shrinkage after sintering.
I would check:
A controlled fill often reduces more scrap than simply raising the pressing force.
3. Use a suitable tooling structure
Single-action pressing may work for simple shapes. Parts with height changes or deep cavities often need floating dies or multi-level punches.
Tool movement should support even pressure through the compact. When one section receives much more force than another, the part may develop lamination, cracks, or uneven density during ejection.
4. Control ejection
Ejection is a common source of damage. A compact that survives pressing can still crack when it leaves the die.
I pay attention to:
A smooth ejection cycle can reduce edge damage and lower the amount of powder sent back for reprocessing.
Powder pressing can use a near-net-shape method. The die forms most of the final geometry, so the process may produce less machining scrap than cutting a part from bar stock.
A practical example is a small bushing. If the die forms the outside diameter, inside hole, and basic height, the process may need only light sizing after sintering. A machined version may start with a larger block and remove a large amount of material.
Powder that remains outside the compact can sometimes be collected and reused. Reuse depends on the powder type, lubricant condition, contamination control, and the quality rules for the product. Powder should not be returned to the process without checking its condition.
“Zero waste” should be treated as a process goal rather than a fixed result. Setup powder, rejected compacts, worn tooling, dust, and off-spec material can still appear.
I would use this sequence when evaluating a 50T powder press:
This approach gives me useful production data before a full batch is released.
Suppose a workshop produces small sintered gears for a light mechanical assembly. The parts have a central hole, shallow teeth, and a moderate height. The team uses a 50T powder press because the required force stays within the machine’s working range.
The first trial shows uneven tooth strength. Raising the load does not solve the problem. A fill test reveals that powder is settling differently near the outer teeth. The team adjusts the fill shoe movement and changes the die lubrication method. The next trial gives a more even compact and fewer damaged teeth during ejection.
The lesson is practical: density problems often begin before the pressing stage. Load is only one part of the process.
A 50T powder press can support efficient powder forming, lower machining waste, and repeatable compaction for suitable parts. Reaching a density close to 99% requires a matched material, die, force, fill method, and sintering cycle. When I see “zero waste” in a process plan, I read it as a target for reducing avoidable loss, not a guarantee that every gram becomes a finished part.
A 50T powder press can help manufacturers improve production speed, repeatability, and material control. Its value depends on more than the press capacity. Product size, powder type, mold design, cycle time, operator skill, and maintenance all affect the result.
Many manufacturers face the same production problems. Manual compaction may create uneven density. A small hydraulic press may struggle with larger parts. A high-capacity machine may take up too much space and raise operating costs. The 50T powder press sits between these options, which makes it suitable for many small and medium-sized components.
The key question is not whether 50 tons sounds powerful. The better question is whether the machine matches the actual forming task.
A 50T powder press applies up to 50 tons of forming force to compact metal powder, ceramic powder, graphite, composite materials, or other suitable formulations. The press places the material inside a die, applies pressure through a punch, and creates a “green” part that can receive further treatment.
Depending on the model, the machine may include:
The same 50T rating can produce different results across different machines. Frame strength, guide accuracy, hydraulic stability, and control quality affect the finished part.
I often see manufacturers focus on maximum force and overlook cycle control. Force matters, but stable pressure and repeatable movement can have a greater effect on daily output.
A 50T powder press may support production in several ways.
Powder parts need controlled density. Uneven pressure can lead to cracks, weak edges, size variation, or poor performance after sintering. A controlled press helps operators repeat the same pressure profile across multiple batches.
This does not remove the need for powder testing. Particle size, moisture, binder content, and lubrication still affect compaction behavior.
A 50T machine usually takes less space than a much larger industrial press. This can help a workshop organize the production line around material storage, mold changes, inspection, and packing.
Space planning should include the full working area, not only the press frame. Operators need room for loading, unloading, maintenance, and safe movement.
A 50T powder press may suit bushings, ferrite parts, small gears, wear components, electrical materials, and simple ceramic shapes. The actual suitability depends on projected surface area and required compaction pressure.
For example, a small workshop producing cylindrical powder components may use a 50T press for low to medium production volumes. The operator can set a repeatable fill weight, compact the powder, inspect the green part, and adjust the mold when density changes appear.
That process can be more stable than relying on hand-operated equipment, while remaining easier to manage than a large multi-station press.
A smaller press may require less installation work, lower power demand, and fewer support systems. This can matter when a business is testing a new product or serving several small orders.
The purchase price should not be the only cost under review. The full calculation should include:
A machine with a lower purchase price may create higher costs if mold changes are slow or pressure control is unstable.
I use a simple review process before selecting a powder press.
Estimate the part’s projected area and required compaction pressure. Add a practical safety margin, then compare the result with the machine’s usable force.
The nominal 50T rating should not be treated as a recommendation for continuous operation at the limit. A supplier should confirm the force calculation based on the material and part design.
The press must accept the required die dimensions, shut height, punch travel, and ejection arrangement. A machine may have enough force but still fail to fit the mold.
Ask for these specifications:
A fast downward stroke does not always produce a fast production cycle. Filling, leveling, pressing, dwell time, ejection, inspection, and loading all use time.
A basic cycle study can show the real output:
This method gives a more useful output estimate than the hydraulic speed listed in a brochure.
Different powders behave in different ways. Fine ceramic powder may require careful venting. Metal powder may need controlled lubrication and dust management. Some materials need a slow pressure build-up to reduce cracks.
The press supplier should review the powder specification, target density, part shape, and post-press process before recommending a machine.
A 50T powder press may not suit large parts with a wide projected area. It may also struggle with complex shapes that need several punches, floating dies, or precise multi-level filling.
Production volume can create another limit. A manually loaded press may work well for prototypes and small batches but become inefficient when orders increase. An automatic feeding system can reduce handling time, though it adds cost and maintenance needs.
Quality control also remains essential. Press pressure alone does not guarantee a usable part. Teams should monitor powder weight, green density, dimensions, surface condition, mold wear, and sintering results.
Powder pressing involves high force and moving tooling. The machine should have suitable guarding, emergency stops, pressure relief protection, and clear operating instructions.
Operators should receive training on:
Maintenance may include checking hydraulic oil, seals, hoses, guides, fasteners, sensors, and electrical connections. Powder dust can also affect moving parts and control cabinets when cleaning is poor.
A clean work area supports stable operation. It also makes small leaks, cracks, and loose components easier to detect.
A 50T powder press can be part of an efficient production plan, but it is not a complete solution by itself. Its value grows when the press works with accurate weighing, suitable tooling, controlled powder preparation, trained operators, and regular inspection.
For a workshop making small or medium-sized powder parts, the machine may offer a practical balance between force, space, control, and operating cost. A company producing large components or high-volume parts may need a larger automated system.
My view is simple: choose the press from the process backward. Start with the material, part dimensions, density target, daily output, and mold design. Compare those requirements with the machine’s usable force and cycle performance. A 50T powder press can support efficient production when the numbers match the application.

Powder waste often begins before the press reaches full load.
A loose fill, uneven feed, or poorly matched tool can leave parts with different densities. Some pieces may crack during ejection. Others may need extra finishing, rework, or disposal. I have seen this happen in shops that focus on press force but overlook the steps around it.
A 50T powder press gives operators a controlled starting point for compacting metal powders, ceramic powders, graphite, and other suitable materials. Its 50-ton nominal capacity can support small and medium-sized components, while the actual result depends on the powder, mold design, fill depth, pressing speed, and target density.
The goal is not to use more force.
The goal is to use the right force with stable material flow.
Where a 50T powder press can help
A 50T machine may suit parts such as:
The machine can help reduce material loss when the tooling matches the part and the powder is fed evenly. A stable pressing cycle also makes it easier to identify where waste occurs.
For example, if a workshop produces small metal bushings and notices cracks along one side, the problem may not come from insufficient pressure. Uneven powder filling can create a density difference across the part. Adjusting the feed system, fill height, or pressing speed may produce better results than simply increasing force.
How I would assess the machine
I would look at the full process rather than judging the press by tonnage alone.
The key points include:
A 50T rating describes the available force. It does not guarantee that every powder or part will reach the required density. A thick component may need a different pressing method from a shallow disc. A brittle ceramic mixture may need slower movement and careful ejection.
Tooling also affects material use. A well-fitted mold can reduce flash, edge damage, and rejected parts. Poor alignment may create uneven walls or make removal difficult. I prefer to test the actual powder and tool combination before selecting a production setting.
A practical setup process
I start with the material.
The powder should have suitable flow, moisture control, and particle distribution for the planned forming method. Small changes in moisture or particle size can affect filling and compaction.
Next, I check the mold.
The cavity should match the intended part size after pressing and sintering. Clearance, surface condition, and alignment all affect part quality. The mold should also allow the compacted part to leave the cavity without excessive force.
Then, I set a trial cycle.
The trial should use a lower, controlled setting rather than the highest available force. I check fill consistency, pressing speed, dwell time, and ejection movement. After pressing, I inspect weight, dimensions, surface condition, and visible cracks.
I also record the results.
A basic production log can include powder batch, fill height, press force, cycle time, part weight, and rejection rate. These records help show whether waste comes from the material, tooling, machine settings, or operator handling.
Waste control starts with measurement
A press may reduce scrap, but only when the process is measured.
I would track:
This creates a clearer picture than looking only at the number of rejected parts. A part may pass visual inspection but still fall outside the required density or dimension range.
Powder recovery also needs care. Recovered material should not be returned to production without checking contamination, moisture, and particle changes. Some materials may require separate handling or disposal based on their safety data and process requirements.
What buyers should ask before purchase
I would ask the supplier for:
A sample test is useful when the part has a complex shape or a narrow density range. It can show whether the 50T powder press is suitable for the application instead of relying on the force rating alone.
The machine should also fit the production space. Power supply, floor strength, ventilation, noise, and access for maintenance can affect the installation plan.
A 50T powder press can support better material control and more consistent compaction for suitable applications. It does not remove every source of waste. Powder preparation, mold design, filling, pressing, ejection, and inspection all influence the final result.
I see the press as one part of a connected process. When the settings are documented and the tooling matches the product, the workshop has a better chance to use powder efficiently, keep density within the required range, and reduce avoidable rework.

When I work with powder compression, two problems appear again and again: the finished tablet lacks the required density, or too much powder is lost during feeding and ejection. A 50T powder press can help address both issues, but the result depends on more than press capacity.
A 50T rating means the machine can apply a maximum compression force of about 50 metric tons, subject to the machine design, tooling, and operating conditions. It does not mean every product should be compressed at that level. Excessive force may cause sticking, capping, lamination, or faster tool wear.
The practical goal is controlled compression:
The powder enters a die cavity through a feed frame or hopper. The lower punch sets the fill depth, while the upper punch moves down to compress the powder bed.
During compression, air leaves the powder mass and the particles move closer together. The final density depends on several factors:
A 50T powder press gives the operator a wider force range than a small laboratory unit. That range can help when a product needs stronger compaction, but force alone does not solve poor powder flow.
I prefer to adjust the material and the machine together. If the powder bridges above the die, adding force will not correct the uneven fill. The press may produce tablets with different weights even when the compression setting remains unchanged.
Powder loss often comes from the feeding stage rather than the main compression stage. Common causes include:
A small amount of loss can affect yield, especially when the active ingredient is costly or the batch size is limited.
A useful way to check the process is to compare the powder charged with the material collected in the tablets, dust collector, rejected tablets, and machine residue. This simple material balance shows where the loss occurs.
1. Check the powder before loading
I review moisture, particle size, bulk density, and flow behavior. Powder that is too damp may stick to the tooling. Powder that is too dry or too fine may create dust and fill the die unevenly.
A short sieve check and a basic flow test can reveal problems before the press starts.
2. Set the feeder for a steady flow
The feeder should move powder into the dies without excessive vibration or scraping. I avoid using a high feeder speed as a quick fix for low output. Fast movement may increase dust, segregation, or uneven filling.
3. Start with a moderate compression force
I produce a small group of tablets and check weight, thickness, hardness, appearance, and disintegration where required. The force can then be adjusted based on the product target.
A denser tablet is not always a better tablet. If the tablet becomes too hard, it may disintegrate slowly or create problems during use.
4. Adjust pre-compression and main compression
Pre-compression can remove part of the trapped air before the main compression step. This may help reduce capping and improve tablet structure.
The main compression stage controls much of the final strength and density. The best setting comes from testing, not from using the full 50T capacity.
5. Inspect ejection
Ejection force gives useful information. A sharp increase may point to excess lubricant, poor tooling condition, unsuitable moisture, or excessive compression.
I inspect the tablet edges and the die wall. Scratched tooling can hold powder and create repeated defects.
6. Record the useful settings
For each product, I record:
These records make later production runs easier to control and help separate material problems from machine problems.
Consider a nutraceutical manufacturer producing mineral tablets. The first trial shows uneven tablet weight and visible powder around the feeder. The operator increases compression force, but the weight variation remains.
The better response is to inspect powder flow and feeder alignment. After improving the powder blend, reducing unnecessary feeder speed, and setting a more stable fill depth, the die cavities receive a more even amount of material. The operator then adjusts compression force to reach the required tablet strength.
The press is part of the solution. The powder preparation and feeding process carry equal weight.
I would ask the supplier for clear information about:
The actual output depends on tablet size, number of stations, material behavior, and operating speed. A 50T powder press may suit one product well and require changes for another.
A high-density tablet with less material loss comes from a balanced process. The press must provide suitable force, while the powder must flow evenly and the tooling must remain clean and aligned. I treat the 50T rating as a working limit, not as a target setting. Careful trials, process records, and regular inspection usually provide a more reliable path to stable tablet production.

Many manufacturers are reviewing 50T powder press technology because production teams need stable compaction, repeatable part quality, and better control over equipment costs. A press with a 50-ton rated force can suit many small and medium powder metal parts, but its value depends on the material, mold design, part size, and required density.
I often see the same production problem: a workshop starts with a small press, then product demand grows. The old machine may struggle with uneven density, slow cycles, or frequent mold adjustments. Moving to a 50T powder press can offer more working capacity without forcing the company to install a large industrial system.
A 50T powder press applies up to 50 tons of pressing force to compact powder inside a mold. The powder may include metal, ceramic, graphite, friction material, or other dry compounds.
During the process, the upper and lower punches compress the material. The compacted shape then leaves the mold and may go through sintering, heat treatment, sizing, or another finishing process.
The rated force is only one part of the machine specification. A buyer also needs to review:
A 50T rating does not mean every part can be made at the same size or density. The actual result depends on how the force is distributed across the pressing surface.
A 50T machine can work well for compact components such as bushings, small gears, ferrite parts, wear-resistant pieces, and selected ceramic products.
For a workshop producing small batches, this capacity may provide enough force for daily production without the space and cost linked to a much larger machine. The machine can support regular orders while leaving room for product changes.
A small automotive component supplier, for example, may use a 50T press to produce simple powder metal spacers. The parts are not very large, but they require stable dimensions and repeatable compaction. A suitable 50T machine can handle this type of work when the mold and powder formula match the equipment.
Manual or poorly controlled compaction often creates differences between parts. Powder filling, pressure, dwell time, and ejection must stay within a controlled range.
A modern 50T powder press may allow operators to set pressure, speed, and stroke values through a control panel. This reduces the need to adjust each cycle by hand. The machine does not remove every production risk, but it can make the process easier to monitor.
I recommend tracking three simple measurements during testing:
These measurements help show whether the press is producing stable results across a batch.
A larger press often requires more floor space, stronger foundations, higher power capacity, and greater mold costs. A 50T powder press may offer a more practical entry point for manufacturers that are expanding production step by step.
This does not mean the lowest purchase price is the right choice. A machine with a lower initial cost may create extra expenses through long setup times, difficult maintenance, or limited mold support.
I look at the full operating picture:
A clear comparison helps prevent a capacity mismatch.
Manufacturers often need equipment that can handle more than one product family. A 50T press may support several molds when the die area, stroke, and ejection system are suitable.
This can help a workshop organize production around shared equipment. One machine may produce several small parts during separate runs, while larger machines remain available for high-force applications.
The changeover process still needs attention. Operators should confirm mold alignment, powder filling settings, pressure limits, and safety checks before starting a new product.
A 50T press is not the right answer for every powder forming task. Large parts, deep shapes, high-density products, or materials with unusual flow behavior may need a different press design or a higher force rating.
The mold also affects the result. A poorly designed die can create cracks, weak edges, or density variation even when the machine has enough rated force.
Before placing an order, I suggest preparing a sample part and sharing these details with the equipment supplier:
A trial run can reveal problems that do not appear in a brochure.
Start by defining the product rather than choosing a machine by tonnage alone. Measure the part size, pressing area, height, and material behavior.
Check whether the 50T press can maintain the required force across the full working stroke. Ask how pressure is measured and how the system responds when the powder filling level changes.
Review the mold installation area carefully. The machine should accept the planned die dimensions and provide enough space for safe adjustment.
Ask for operating samples or test data from a similar application. The sample should show more than a finished appearance. Part weight, density, dimensional variation, cycle time, and ejection quality provide better guidance.
Speak with the service team about common wear parts. Seals, sensors, hydraulic components, control elements, and mold accessories can affect production uptime.
Train operators before regular production begins. They need to understand pressure settings, powder handling, mold inspection, emergency stops, and basic fault checks.
Manufacturers are turning to 50T powder press technology because it can match the needs of many small and medium components without creating an oversized production setup. The best result comes from matching the press to the powder, mold, part size, and production plan.
A 50T rating offers useful capacity, but it is not a guarantee of quality by itself. Careful testing, suitable tooling, and steady process control decide whether the equipment becomes a productive part of the workshop.
Contact us on Hu: dgliheng168@163.com/WhatsApp +8613509684273.
References
European Powder Metallurgy Association 2023 Powder Metallurgy Design and Production Principles
German 2022 Compaction Behavior and Density Control of Metal Powders
World Powder Metallurgy Association 2021 Advances in Powder Compaction Technology
Smith 2020 Tooling Design and Ejection Control for Powder Pressing
Johnson 2019 Material Efficiency and Waste Reduction in Powder Metal Manufacturing
International Organization for Standardization 2018 Metallic Powders Determination of Apparent Density and Flow Rate
Stop wasting money on excessive energy costs. The 50T press can reduce energy consumption by up to 30%, helping lower operating expenses while maintaining reliable performance. By upgrading to this
Roll smarter, not harder with Shengshi—your trusted partner in efficient, reliable, and innovative rolling solutions. Designed to enhance performance, streamline operations, and simplify every st
Tired of inaccurate rolls and inconsistent results? Try this solution to improve precision, enhance reliability, and enjoy a smoother overall experience. Designed to reduce errors and deliver more
Flawless curved steel plates are the result of precision engineering, carefully controlled forming techniques, and rigorous quality assurance. From accurate material selection and advanced bending
Email to this supplier

November 11, 2026

October 21, 2026
Contact

Send Inquiry
PRODUCT CATEGORIES
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.