
Send Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
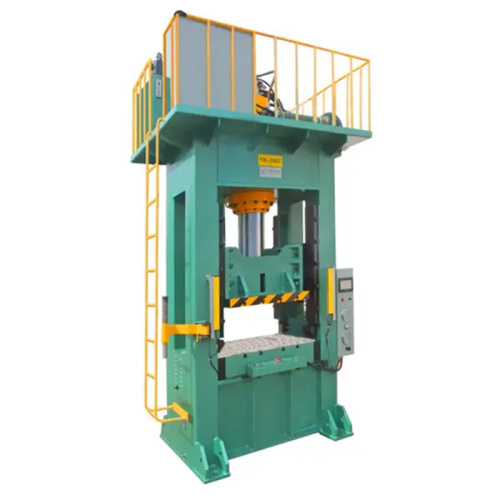
50T powder molding technology provides the controlled force and stability needed to produce precise, reliable powder compacts for demanding manufacturing applications. By applying up to 50 tons of accurately regulated pressure, the system promotes uniform material distribution, consistent density, and strong bonding throughout each molded part. This helps reduce porosity, dimensional variation, cracking, and production waste while improving repeatability from one cycle to the next. Advanced control over pressure, dwell time, and mold alignment further enhances accuracy, enabling manufacturers to create components with smooth finishes, dependable mechanical strength, and tight tolerances. From industrial parts and automotive components to specialized technical products, 50T powder molding offers an efficient and dependable path to higher-quality compacts, combining robust performance with consistent production results.

A 50T powder molding press can turn loose powder into strong, repeatable compacts, but the press alone does not decide the result. Powder flow, die design, filling depth, compression pressure, dwell time, and ejection all affect the finished part.
I have seen many operators focus only on the 50-ton rating. They expect every mold to produce dense, accurate parts. The common problem is simple: press capacity and molding pressure are not the same thing.
A 50T press provides a maximum force of about 490 kN. The pressure applied to the powder depends on the projected area inside the die.
Pressure = Compaction Force ÷ Pressed Area
A small part may receive high pressure from a 50T machine. A larger part may receive much less pressure because the force spreads across a wider area. This calculation should guide mold size, part dimensions, and powder selection before production begins.
Powder must flow into the die cavity with as little variation as possible. Poor flow can create air pockets, uneven density, and weak edges.
Check these points before loading the press:
Powder that absorbs moisture may stick to the punch or form uneven fills. Powder with poor flow may leave the cavity partly empty. Both conditions can produce parts that look acceptable on the surface but break during handling or later processing.
I prefer to test a small batch before setting up a full production run. A short trial can reveal filling problems without using a large amount of material.
The mold controls the shape, dimensions, and release behavior of the compact.
A practical die should include:
Sharp internal corners may create stress points in the compact. A small radius can improve powder movement and reduce chipping during ejection, depending on the product design.
The mold should also allow the operator to clean powder residue easily. Fine powder can collect around the die and affect the next filling cycle.
Filling height has a direct effect on part weight and density. If the powder level changes from one cycle to the next, the compact weight will change as well.
I recommend using a fixed filling method rather than relying on visual judgment. A measured feeder, controlled shoe movement, or set filling stroke can make each cycle more consistent.
Record the following during setup:
These records help identify the source of variation when a batch does not meet the required standard.
A fast compression stroke may trap air inside the powder. It can also create cracks, edge damage, or uneven density.
A controlled cycle often works better:
The correct settings depend on the powder and part shape. I would not copy a pressure value from another material without testing it. Metal powder, ceramic powder, graphite, and pharmaceutical materials can behave very differently.
The 50T label describes the maximum press force. It does not mean the machine should run at maximum force for every part.
Running near the limit may increase wear on the frame, hydraulic system, tooling, and punches. The machine manual should define the safe operating range. The mold must also withstand the selected load.
Before production, check:
A mold that fits on the table may still be unsuitable if the stroke or daylight is too short. Alignment matters as well. Uneven loading can damage punches and create non-uniform parts.
Imagine a small workshop producing cylindrical powder compacts for a later heating process. The operator uses a 50T press and notices that some pieces crack during ejection.
The first reaction may be to increase the pressing force. That may not solve the issue.
A better check would include:
If the part weight varies, the filling process may be the main cause. If the weight is stable but the compact cracks during release, friction, punch alignment, or ejection speed may need attention.
This type of step-by-step check helps prevent random setting changes.
A compact can look smooth and still have internal weakness. Quality checks should match the product requirement.
Useful checks may include:
For repeat production, take samples at different points in the run. A part made at the start of a batch may not match one made after several hours if powder flow, temperature, or tooling condition changes.
Keep inspection results with the press settings. This creates a useful reference for future batches without treating one setting as suitable for every material.
Using the maximum force for every product
More force does not always produce a better compact. Excessive force can damage the mold or make ejection harder.
Changing several settings at once
When pressure, filling amount, speed, and dwell time all change together, it becomes hard to identify what improved or harmed the part.
Ignoring ejection
Many defects appear after compression. A compact may form correctly and crack when the punch pulls it from the die.
Skipping powder preparation
Uneven powder condition often leads to uneven part density. Press adjustments cannot fully correct a poor feedstock.
Treating every powder in the same way
Each powder has its own flow, friction, compressibility, and moisture response. A setup that works for one material may fail with another.
A simple operating sheet can improve consistency across shifts. I would include:
The sheet does not need to be complex. Clear records help operators make measured adjustments instead of relying on memory.
A 50T powder molding press works best when the machine, powder, mold, and process settings are treated as one system. Calculate the required pressure, control the fill, protect the tooling, and inspect the compact after ejection.
Strong, clean compacts come from stable process control rather than force alone.

A powder compact can look fine on the outside and still fail after ejection, sintering, or machining. Uneven density, edge cracks, weak corners, and size changes often begin during pressing. I have found that the problem is rarely the press force alone. Powder flow, die filling, tooling condition, moisture, dwell time, and force control all affect the result.
A 50T powder molding press gives manufacturers a useful working range for small and medium-sized parts. When the machine, powder, and tooling match the application, the press can produce compacts with more stable shape, repeatable weight, and improved green strength.
A 50T machine can apply a maximum pressing force close to 50 metric tons, subject to the machine design and operating conditions. This force is distributed across the projected area of the part.
A small compact may receive high pressure with a lower total force. A larger compact may need more force to reach the same pressure level. For this reason, I do not judge a press only by its tonnage. I check the target pressure, part area, powder behavior, and tool design together.
The calculation is simple:
Compaction pressure = pressing force ÷ projected area
This helps engineers select a suitable machine before they build the die. It can prevent a common mistake: choosing a press by tonnage alone and finding that the finished part still has low density.
The pressing cycle starts before the upper punch moves. The die cavity must receive a stable powder charge. Poor filling can leave one side of the part heavier than the other. The compact may then show density variation, lamination, or uneven shrinkage during sintering.
I pay close attention to:
A free-flowing granulated powder usually fills the cavity more evenly than a powder with poor flow. Deep cavities may need controlled filling or several feed actions. A small change in fill height can affect compact weight and final dimensions.
A 50T powder molding machine can help maintain a steady pressing cycle when its hydraulic or servo system responds consistently. Stable force control supports repeatable compact height and green density.
I prefer to set the cycle around the material instead of using one pressure value for every powder. The machine may use a gradual pre-press, a main pressing stage, and a short dwell. This gives trapped air more time to escape and lets the powder structure settle under load.
The correct settings depend on the material. Ceramic powders, metal powders, graphite blends, and carbide mixtures do not respond in the same way. A pressure that works for one formula may create cracking or sticking in another.
The die and punches transfer the 50T force into the powder. Any gap, wear mark, poor surface finish, or misalignment can affect the compact.
I check the following areas during setup:
Sharp internal corners often create stress points. A suitable radius can reduce corner damage, though the radius must fit the part design. Ejection speed needs attention as well. If the compact leaves the die too quickly, friction can create cracks even when the pressing stage looks stable.
Consider a line producing small ceramic wear blocks. The operator notices that several pieces crack after ejection. The press reaches the required force, but the defect continues.
I would review the full cycle rather than raise the force immediately. The powder feed may be uneven. The die wall may have excess friction. The dwell period may be too short. The ejection motion may be too fast. Moisture may have changed after storage.
A controlled trial can compare:
The team can then test green strength, density distribution, and sintered dimensions. This approach gives more useful information than changing several settings at once.
Press force is only one process result. I use several checks to understand whether the compact is stable:
A simple weight and height check can reveal fill variation early. Density testing can show whether the center and edges are receiving similar compaction. When the part is critical, section analysis or internal inspection may be needed.
Process records help link defects to machine settings. I record powder batch, fill setting, force curve, dwell time, ejection speed, and tool condition. This makes troubleshooting more direct when a defect appears after a material change.
A 50T powder molding press suits many small components, test batches, replacement parts, and medium-volume production jobs. It may not suit every large part or high-density material. The correct choice depends on the required pressure, projected area, cycle design, die size, and production rate.
I recommend confirming these points before purchase or installation:
A machine with enough force but poor control may produce less consistent results than a lower-force machine with a stable cycle and suitable tooling.
The main lesson is simple: a 50T powder molding press can deliver better compacts when the full process is controlled. Balanced filling, suitable pressure, steady dwell, careful ejection, and sound tooling work together. I treat the press as one part of the production system, not as the only answer to density or cracking problems.

A good powder compact starts long before the press closes.
When I work on a pressed powder project, I focus on more than appearance. The powder needs to fill the pan evenly, hold its shape during use, release the right amount onto a brush, and stay secure inside the case. A smooth surface means little if the product cracks during transport or feels too hard on the skin.
A reliable process helps solve these problems step by step.
The formula affects every later stage of production.
I check the particle size, oil level, pigment load, and binding system before choosing a pressing method. A face powder, blush, bronzer, and eyeshadow may all look similar in a compact, yet each one can need a different balance of ingredients.
A formula that contains too much oil may feel heavy or form marks on the surface. A formula with too little binder may break when the compact is dropped. Highly pigmented shades can also need careful mixing to prevent uneven color.
A useful test is to press a small batch and check:
I prefer to solve formula issues before large-scale production. Small trial batches make it easier to adjust the binder, pressure, or filling method without creating large amounts of waste.
The metal pan should match the formula and the compact design.
Common materials include aluminum and tin-plated steel. The choice depends on the product type, pan size, filling method, and expected use. The pan also needs the right depth. A shallow pan may make the powder look full but can increase the chance of damage. A deeper pan may protect the product but reduce the space available inside the case.
I also check the pan surface before filling. Dust, oil, or uneven coating can affect adhesion. If the powder does not bond well with the pan, it may lift when the customer uses a brush or sponge.
The compact should close without pressing against the powder. A mirror, divider, or inner lid that sits too close can leave marks on the surface.
Uneven filling often leads to uneven pressing.
I use a controlled filling method to spread the powder across the full pan area. The goal is to avoid empty corners, air pockets, and thick spots. Some formulas need light pre-compression before the main press. This step can help remove trapped air and improve the final surface.
The filling weight needs regular checks. A simple scale check during production can show whether the powder amount is staying within the agreed range. The target should be based on the product specification, not on visual judgment alone.
When the powder is filled, I inspect the pan from several angles. A compact may appear full from above while still having a low area near the edge.
Pressing pressure affects texture, strength, and pickup.
Too much pressure can create a hard cake that gives little color to a brush. Too little pressure can leave a fragile cake that breaks during handling. The right setting depends on the formula, pan size, powder depth, and binder.
I test several pressure levels with the same batch of powder. Each sample is checked for:
A practical example is a matte blush that looks smooth after pressing but gives almost no color when applied. In that case, reducing pressure may improve pickup. A powder that breaks around the edge may need better filling control, a small formula adjustment, or a different pressing setting.
The surface should look even without cracks, dents, or loose powder around the edge.
Color checks need to take place under stable lighting. I compare the pressed product with the approved color standard rather than relying on memory. This matters more with pale shades and high-pigment products, where small changes can be easy to see.
For multi-shade palettes, I keep each shade separated during filling and cleaning. A small amount of dark pigment can change a light shade. Clean tools and clear batch labels help reduce this risk.
The powder and the case need to work together.
I check the hinge, clasp, mirror, pan fit, and inner tray. The compact should open and close smoothly without causing pressure on the pressed powder. I also inspect the product after basic transport tests, such as vibration, repeated opening and closing, and controlled drops based on the project standard.
These tests do not replace local safety and quality requirements. They give the production team useful information about weak points before shipment.
Packaging also affects customer experience. A compact that becomes dusty around the edges may need a better cleaning step before assembly. A loose pan may need a stronger adhesive or a tighter tray design.
A powder compact becomes easier to repeat when the process is documented.
I record the formula version, pan size, filling weight, pressing setting, production date, packaging batch, and inspection results. Photos of approved samples can help the team compare future batches with the original standard.
When a problem appears, clear records make the cause easier to trace. Without them, the team may change several factors at the same time and lose the link between the adjustment and the result.
A consistent powder compact comes from several small controls working together. The formula, pan, filling weight, pressing pressure, case design, and inspection process all affect the finished product. I do not treat a smooth surface as the only sign of quality. A well-made compact should also provide stable color, balanced pickup, secure packaging, and a pleasant daily use experience.

When a powder molding line produces parts with different weights, heights, or surface quality, the press size is not always the main problem. Powder condition, filling accuracy, mold design, pressure control, and ejection timing all affect the result.
A 50T powder molding press can produce stable parts when these factors work together. I see the best results when the machine is used within its working range and the process is measured at each stage, rather than relying on pressure alone.
A 50T press provides a controlled forming force
The “50T” rating refers to the maximum forming force of the press. It gives the mold enough pressure to compact many small and medium-sized powder parts, such as ceramic pieces, ferrite components, friction parts, and certain metal powder products.
The press does not need to operate at its maximum load for every part. When the required force is well matched to the product size and material, the machine can run with less strain and better control. This helps reduce changes in:
I usually recommend calculating the required forming force from the projected area, target pressure, and powder type. A part that needs only a moderate load should not be forced through a process designed around the press limit.
Stable powder filling supports stable part weight
A powder press can repeat the same pressure, yet the finished parts may still vary if each mold cavity receives a different amount of powder.
Powder flow depends on particle size, moisture, additives, shape, and storage conditions. A free-flowing powder may fill the cavity quickly, while a powder with poor flow can leave air pockets or uneven areas.
The process becomes more stable when the operator controls:
For example, when producing small ferrite cores, a small difference in powder weight can affect the finished height and density. A controlled feeder and a steady hopper level help each cavity receive a similar charge before pressing starts.
Mold design affects the final result
The press creates force, but the mold determines how that force reaches the powder.
A well-designed mold can guide the powder evenly and support smooth movement during compression. Poor alignment may create uneven density, chipped edges, or extra wear on the tooling.
I pay close attention to:
Venting also matters. Air trapped inside the powder may lead to cracks, delamination, or weak areas. A slower pre-press stage can give the trapped air a path to escape before the main compression takes place.
Pressure alone does not control density
Many operators focus only on the pressure number shown on the machine. I treat pressure as one part of the process.
The pressure curve, hold time, filling amount, and punch movement can all change the compacted structure. Two parts made at the same peak pressure may show different results if one receives a short hold and the other stays under pressure for longer.
A controlled cycle may include:
This sequence gives the powder time to settle and reduces sudden stress inside the compact. The correct settings depend on the material and part design, so the process should be confirmed through sample testing.
Ejection needs the same level of control
Some defects appear after pressing rather than during compression. A part may look acceptable inside the mold but crack when the punch rises or the ejector moves too quickly.
A controlled ejection speed can reduce:
Lubrication may also help, though the amount must match the material and product requirements. Excess lubricant can change density or affect later heating and sintering steps.
Why 50T works well for many production setups
A 50T press often fits small and medium production tasks because it offers enough force for many compact parts without requiring a large machine footprint. It can also support easier tool changes, lower energy use, and simpler operator access when the product size is suitable.
A practical example is a small batch of pressed ceramic spacers. If the cavity is filled with a controlled powder charge, the mold is aligned, and the press uses the same pressure and dwell time for each cycle, the parts can show a narrow variation in height and weight. If the same batch is produced with an unstable powder feed, the 50T rating alone will not correct the problem.
I prefer to confirm consistency with simple checks:
These records help identify the source of variation before it affects a large batch.
Consistent results come from the whole process
The reason 50T powder molding can deliver consistent results is not the tonnage by itself. The result comes from matching the press, mold, powder, and operating settings to the product.
When I evaluate a powder molding process, I look at the complete cycle. A stable powder charge, accurate tooling, controlled pressure, steady ejection, and regular inspection usually have more influence than a larger press rating.
A 50T machine can be a practical choice for many powder molding applications when the product falls within its force and size range. The most reliable setup is the one supported by measured data, repeatable settings, and a mold designed for the material being pressed.

A 50T powder molding press can help manufacturers produce compact parts with steady pressure, controlled size, and a practical production rhythm. The press size alone does not decide the result. Powder type, die design, filling method, pressing speed, and inspection all affect the finished compact.
I look at these factors together when choosing a 50T powder molding solution.
Many buyers face a similar problem: the press can reach the required force, yet the compact still shows cracks, uneven density, edge damage, or size variation. These issues may appear during pressing, ejection, sintering, or final inspection. A suitable machine should support the full process instead of focusing on tonnage alone.
A 50T press is often considered for small and medium powder parts, such as:
The correct application depends on the powder, part shape, projected area, target density, and required output.
I start with the part’s projected area and the powder’s pressing pressure. A rough calculation can help confirm whether 50 tons is suitable:
Required force = projected area × compacting pressure
The result should include a suitable safety margin. A part with a small footprint may work well on a 50T machine. A wider part, a deep cavity, or a product requiring high density may need a larger press or a different process.
The calculation should also consider:
A machine that operates near its maximum capacity for every cycle may experience more wear and may offer less process flexibility.
Different powders behave in different ways. Iron-based powder, copper-based powder, ceramic powder, and magnetic powder may require different filling and pressing settings.
I check whether the system can support:
Powder flow has a direct effect on density distribution. If the die does not fill evenly, the compact may have weak areas even when the pressure reading looks normal.
A reliable compact starts with a suitable die. The die should match the part geometry and allow the powder to fill the cavity without excessive friction.
For a new project, I review:
A simple cylindrical bushing may be easier to press than a part with thin walls, narrow slots, or several height levels. Complex shapes may need multiple punches or a staged pressing method.
The pressure value is only one part of the process. Punch position, pressing speed, dwell time, and ejection speed also affect the compact.
A useful setup may include:
When I review a machine, I prefer controls that operators can understand without a long learning period. Clear settings reduce setup mistakes and make it easier to compare results between batches.
The green compact should be checked before sintering. Early inspection can prevent a larger batch of defective parts.
Common checks include:
For example, a plant producing small powder bushings may find that the outer diameter is within range while the weight varies between pieces. This can point to uneven filling or inconsistent powder flow rather than a simple pressure problem. Adjusting the feeder and filling depth may bring the batch closer to the target than increasing the press force.
A press used for powder molding needs a practical maintenance plan. Powder can enter moving areas, sensors, guides, and working surfaces. Regular cleaning helps reduce buildup and supports stable operation.
I would check:
A machine that is difficult to clean may increase changeover time and raise the risk of powder cross-contamination.
A 50T powder molding press can be a suitable option for many compact parts, but the decision should come from process data rather than the tonnage label. I would prepare the part drawing, powder details, target density, expected cycle rate, and inspection requirements before asking for a machine proposal.
A useful supplier discussion should cover:
If possible, test the actual powder and die concept before placing an order. A short sample run can reveal filling, cracking, ejection, and dimensional issues that may not appear in a basic machine specification.
The right 50T powder molding setup is not defined by force alone. It should give the operator control over filling, pressing, ejection, and inspection while fitting the material and part design. When these details are reviewed together, manufacturers can build compact parts with more consistent results and a clearer production plan.
For any inquiries regarding the content of this article, please contact Hu: dgliheng168@163.com/WhatsApp +8613509684273.
Richard W Lewis, March 15, 2021, Fundamentals of Powder Compaction and Pressing
Elena M Carter, July 8, 2020, Die Design and Density Control in Powder Molding
Michael T Brooks, November 22, 2022, Process Parameters for Reliable Powder Compacts
Sophia R Bennett, April 17, 2019, Powder Flow Filling Accuracy and Compact Quality
Daniel K Morgan, September 5, 2023, Ejection Control and Defect Prevention in Pressed Powder Parts
James A Turner, January 26, 2024, Practical Applications of 50T Powder Molding Presses
Before buying a 50-ton press, take a closer look than the tonnage alone. The right machine should match your production needs, material requirements, tooling, and expected workload. Evaluate its tr
The 50T Press combines powerful 50-ton force with an ultra-fast 10-second cycle time, delivering consistent, high-precision results in every operation. Designed for demanding production environment
Is your old 50-ton hydraulic press truly obsolete? Not necessarily. If it still delivers reliable pressure, consistent results, and acceptable cycle times, it may remain a practical choice for basi
Discover why 80% of factories are switching to our 50T press. Engineered for demanding production environments, it combines powerful performance, reliable operation, high precision, and energy-effi
Email to this supplier

November 15, 2026

November 14, 2026
Contact

Send Inquiry
PRODUCT CATEGORIES
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.