
Send Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
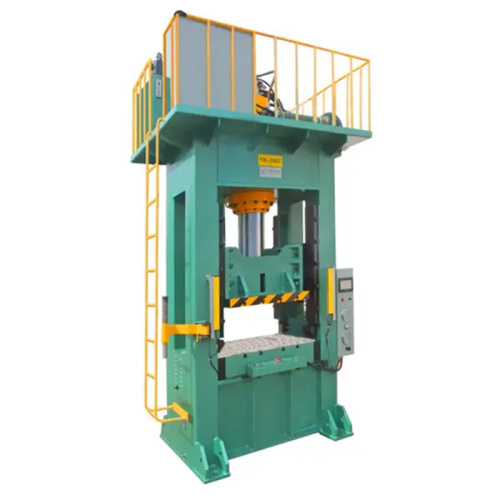
The truth about 50T powder presses is that their value depends on more than nominal pressing force. With a maximum capacity of 50 tons, these machines can deliver consistent compaction for a wide range of powder-based components, including ceramics, metal parts, friction materials, and industrial products. Their key advantages include reliable pressure control, repeatable forming results, efficient production, and compatibility with various molds and automation systems. However, performance also depends on material characteristics, mold design, stroke length, cycle speed, and operator expertise. A 50T press may be ideal for small- to medium-sized components and moderate production volumes, but it may not meet the requirements of oversized parts, exceptionally dense materials, or high-speed mass manufacturing. Manufacturers should evaluate precision, energy consumption, maintenance needs, safety features, and total operating costs before investing. In short, a 50T powder press offers a practical balance of power, flexibility, and efficiency, provided its capabilities match the specific demands of the production process.


A 50T powder press can look like a strong and flexible machine on a product page. I understand why many buyers focus on the force rating first. The number is easy to compare, while the details that affect daily production often sit in the fine print.
I have seen buyers choose a 50-ton powder press for a die size, powder type, or production target that the machine was not designed to handle. The press may reach the stated force, yet the finished parts can still show cracks, density changes, sticking, or uneven edges.
The force rating is only one part of the decision.
50T does not mean 50 tons of useful pressure everywhere
A 50T powder press usually refers to its maximum pressing force. It does not tell me the pressure applied to each square millimeter of the powder.
Force, die area, powder height, filling method, tooling strength, and pressing speed all affect the result. A large die spreads the force across a wider area. A small die creates a different pressure pattern. The same machine can produce different results when the tooling or powder changes.
I also need to check whether the 50T rating is:
These details affect equipment life and production stability. A machine that reaches 50T for a brief test may not be suitable for repeated cycles at that load.
The powder decides more than many buyers expect
Metal powder, ceramic powder, graphite, pharmaceutical material, and recycled compounds do not behave the same way.
Some powders flow well into the die. Others form bridges, hold air, or separate by particle size. Moisture can change filling behavior. Lubricant can improve ejection, yet too much lubricant may affect strength or surface quality.
A small ceramics workshop, for example, may use a 50T press to form test pieces or small production parts. The operator may notice that two parts with the same weight have different strength. The cause may not be the press force. Uneven powder filling or trapped air can create density differences inside the part.
I would ask for test pressing with the actual powder before placing an order. A sample using a seller’s standard material cannot show how my own powder will perform.
Useful test details include:
A test report should include numbers and photos, not only a statement that the sample “worked.”
Tooling is often the hidden cost
The press may be affordable while the tooling costs more than expected. A powder press needs suitable dies, punches, guides, spacers, and sometimes a special ejection system.
The tooling must handle the planned force without bending, cracking, or wearing too quickly. Its material, heat treatment, surface finish, and alignment all matter.
I would not accept a general answer such as “the die is included.” I would ask:
A poorly aligned punch can damage the die and create uneven parts. It can also increase operator risk. The frame, guides, and tooling should work as one system.
Single-action and double-action pressing produce different results
A single-action press applies force from one side. This setup may be suitable for simple, thin parts. Taller or denser parts can show more variation because the powder near the pressing surface receives a different force from the powder farther away.
A double-action system presses from both sides. It may improve density distribution for certain shapes, but it also adds cost, controls, and setup work. It does not solve every powder problem.
My choice would depend on the part height, shape, density target, and acceptable variation. A seller who recommends a press without asking about these points may be using the tonnage as the main sales argument.
Cycle time needs a closer look
A product page may show the maximum stroke or motor power, but that does not tell me the complete cycle time.
A powder pressing cycle may include:
The press may move quickly while the operator still spends most of the cycle preparing the powder and removing the part. Manual loading can limit output more than the machine itself.
For a small batch operation, this may be acceptable. For repeated production, I would measure the full cycle with the actual tooling and operator process. I would also check whether the machine can maintain the same force and stroke after several hours of use.
Hydraulic details deserve attention
Many 50T powder presses use hydraulic systems. The pump, valve, cylinder, oil tank, cooling method, and pressure control affect performance.
I would ask about:
A machine can operate well during a short demonstration and show pressure drift after continuous use. Pressure drift may change part density from one batch to another.
The control system also matters. A basic pressure gauge may be enough for simple work. A digital controller with adjustable dwell time and stroke limits gives better process control, but it may require more training and maintenance.
Safety should be checked before the price
A 50T press stores and releases a large amount of force. I would check the guarding, emergency stop, two-hand controls, access around the die, overload protection, and electrical wiring.
The operator should not need to place hands near the tooling during normal loading or ejection. The machine should have clear operating instructions and maintenance points.
If the press will be used with fine metal or organic powders, dust control also matters. Powder dust can affect breathing, housekeeping, electrical components, and fire risk, depending on the material. The press supplier should provide material-specific safety information rather than a general statement that the machine is safe.
The advertised price may not be the purchase price
A low machine price may exclude several items:
I prefer to request a complete quotation with each item listed. This makes it easier to compare two machines that appear similar.
A supplier should also explain the warranty in plain language. I would check whether the warranty covers the pump, cylinder, controls, frame, seals, and tooling. Wear parts may have different coverage.
Questions I would send before ordering
I would ask the seller to answer these points in writing:
Clear answers usually reveal more than a large force number.
A 50T powder press can be a practical choice for small parts, test work, and selected production tasks. It is not automatically suitable for every powder or die size. I would judge the machine by the complete process: filling, pressing, holding, ejection, inspection, maintenance, and operator safety.
The press should match the part and the powder. When I compare machines this way, the purchase becomes less about the biggest number on the brochure and more about producing consistent parts with manageable operating costs.

A 50T powder press can produce useful results, but its rated force does not tell the whole story. Many buyers look at “50T” and expect the same output from every machine. The actual result depends on powder type, mold size, filling method, pressing speed, pressure control, and ejection design.
I look at a powder press through one practical question: can it produce stable parts under the conditions of the intended job?
A 50T press usually provides a maximum force close to 490 kN. That figure describes pressing capacity, not guaranteed product quality. A larger mold area spreads the force across more surface. A small die can receive higher pressure from the same machine, while a large die may need more force to reach the target density.
The basic relationship is:
Pressure = Pressing force ÷ Pressing area
A buyer should calculate the required force from the projected area of the part and the pressure needed by the powder. The calculation should include a suitable operating margin. Running a machine at its limit for every cycle can place more load on the frame, hydraulic system, tooling, and seals.
Powder flow has a direct effect on filling accuracy. Powders with uneven particle size, poor flow, or high moisture can create gaps inside the die. The press may reach the selected force, yet the finished part can show density differences, cracks, or weak edges.
Particle size distribution matters as well. Fine powder can improve surface detail but may need better ventilation and stronger compaction. Coarser powder may fill faster, though it can leave a rougher surface or lower density in certain shapes.
Binder content changes the way powder behaves under load. Too little binder can make green parts fragile. Too much binder can affect shrinkage, surface quality, or later heating. Each material needs its own trial settings.
The mold has an equal role. A strong press cannot correct a poorly designed die. Clearance, punch alignment, wall finish, and ejection movement all influence the result. If the upper and lower punches do not move evenly, the part may have different density from one side to the other.
Pressing speed affects how air leaves the powder. A fast stroke can trap air, especially in fine powders. A controlled dwell period at peak force gives the material more time to settle. The best setting depends on the powder and shape, not only on the machine’s maximum cycle speed.
I do not judge a press only by its maximum tonnage. I check five areas:
Force stability is easy to overlook. A pressure gauge may show the target value, but the actual force can fluctuate if the hydraulic system, relief valve, or pump is not working smoothly. A digital pressure sensor or load cell can provide more useful data during testing.
Part weight gives a quick indication of filling consistency. It does not replace density testing, but it helps identify changes in powder flow or die filling. If the weight moves outside the accepted range, the operator should inspect the feeder, powder preparation, and mold condition before changing the pressure alone.
Density testing gives a deeper view. A part may have the correct weight while still containing uneven areas. For ceramic, metal, graphite, or other compacted materials, samples can be checked at several positions. The result helps show whether the pressure reaches the full part evenly.
Ejection needs close attention. A part that looks correct after pressing can crack when the punch removes it from the die. High ejection force may point to poor wall finish, excessive compaction, insufficient lubricant, or a mold alignment issue.
A small ceramic bushing workshop may use a 50T hydraulic press for simple ring-shaped parts. The operator may notice cracks around the inner wall after ejection. Raising the pressure seems like a natural response, but it can make the problem worse.
A better check starts with powder moisture, lubricant level, die wall condition, and punch alignment. The operator can then compare several test settings:
If the cracks reduce after these changes, the problem was not a lack of pressing force. It came from the interaction between powder behavior, mold friction, and ejection.
This type of case appears in many powder forming jobs. The same 50T machine can perform well on a small ferrite component and deliver poor results on a larger ceramic plate because the pressing area, powder flow, and air release path are different.
I recommend a short test plan before a machine enters regular production.
Step 1: Define the part
Record the part diameter, height, wall thickness, target weight, target density, and expected production rate. Note whether the part has holes, steps, ribs, or thin edges.
Step 2: Calculate the force
Estimate the required force from the projected pressing area and material pressure. Check whether the calculated load sits below the machine’s practical working range.
Step 3: Prepare one powder batch
Keep moisture, binder, lubricant, and particle size as consistent as possible. Changing the powder and machine settings at the same time makes the test difficult to read.
Step 4: Run several pressure settings
Use a controlled range rather than jumping directly to the maximum setting. Record pressure, dwell time, cycle time, part weight, appearance, and ejection force.
Step 5: Check the parts
Measure weight and dimensions. Inspect edges, corners, holes, and surface marks. Use density checks when the material requires tighter control.
Step 6: Repeat the test
Run enough cycles to show whether the result stays stable. A few good pieces do not prove production consistency. A longer run can reveal oil temperature changes, seal problems, powder segregation, or tool heating.
The frame should match the expected force and working conditions. Ask for information about maximum force, working force, stroke length, daylight, table size, pressing speed, return speed, and ejection capacity.
The control system deserves attention. A machine with adjustable pressure, dwell time, and stroke position gives the operator more control over powder behavior. A pressure-only system may be suitable for simple parts, but it can offer fewer ways to correct density variation.
Tooling space must fit the mold. A 50T machine may have enough force but not enough daylight or table area for the planned die set. Check the distance between the platens, mounting holes, punch travel, and access for loading and unloading.
Safety features should be part of the purchase check. Guarding, emergency stops, pressure relief, two-hand controls, and safe access around the mold protect the operator during setup and production. These features support daily use and should not be treated as optional decoration.
Maintenance access affects long-term operation. Operators should be able to inspect hydraulic oil, filters, hoses, seals, guides, and electrical parts without taking apart large sections of the machine. Clean oil and aligned tooling help maintain stable performance.
Using maximum force for every material can shorten tool life and increase the chance of cracks. More force does not always create a better part.
Changing several settings at once makes troubleshooting harder. I prefer to adjust one factor, record the result, and compare the next sample with the previous one.
Ignoring powder preparation can lead to false conclusions about the press. A well-built machine cannot compensate for inconsistent moisture, poor mixing, or uneven particle flow.
Choosing a press by tonnage alone can create a poor fit. A machine with suitable force but limited stroke, small table space, or weak ejection control may not meet the needs of the actual part.
A 50T powder press can be a practical choice for small and medium powder forming tasks when the force, tooling, material, and control settings match the job. Its performance should be judged through stable cycles, consistent parts, controlled ejection, and repeatable test data.
The most useful buying decision comes from testing the intended powder and mold together. The number printed on the machine matters, but the quality of the finished part shows whether the press truly fits the process.
A 50T powder press can look suitable on paper, yet the number alone does not tell me whether the machine will fit my production needs.
When I compare powder presses, I look beyond the advertised force. The material, mold size, working speed, pressure control, feeding method, maintenance needs, and after-sales support all affect the result. A press that works well for ceramic powder may not be suitable for metal powder, graphite, herbal materials, or recycled compounds.
The right choice starts with the powder and the finished product.
“50T” usually refers to a maximum pressing force of 50 tons. It does not automatically describe:
I always ask the supplier to provide the full working range, not only the maximum force.
A useful question is:
Can the machine apply stable pressure at the level I need for my product?
Some materials need less pressure but better control. Others need a longer holding time to reduce cracks or improve density. If the machine only offers a high peak force without steady control, the finished parts may show uneven density.
Different powders behave in different ways.
Metal powder may need controlled filling, strong tooling, and careful pressure release. Ceramic powder can be sensitive to moisture and may crack if the pressure changes too quickly. Herbal or chemical powders may need food-grade or corrosion-resistant contact parts. Graphite and other fine powders may create dust that affects the working area and machine components.
Before I request a quotation, I prepare these details:
A supplier should be able to review these points before suggesting a model. If the conversation stays focused only on price and tonnage, I treat that as a sign to ask more technical questions.
The required force depends on the pressing area and the pressure needed for the material.
A simple reference formula is:
Pressing force = pressing area × required pressure
The actual calculation may also involve product shape, friction, powder flow, mold design, and the way force is applied. A round tablet, a simple block, and a deep part can require very different tooling conditions.
For example, a small product with a large pressing area may need more force than a taller product with a smaller area. A 50T press may be suitable for one mold but too limited for another.
I ask the supplier to show the calculation or testing basis. A clear answer is more useful than a general statement that the machine is “strong enough.”
The mold often affects production more than the press itself.
I check whether the machine supports:
A poorly designed mold can cause sticking, edge damage, inconsistent weight, and difficult demolding. These problems may continue even when the press has enough force.
I also ask about mold life. The answer should depend on the powder, pressure, cycle rate, mold material, and maintenance method. A supplier should avoid giving one fixed service-life number for every application.
A stable pressure system helps control product quality.
I want to know:
A manual hydraulic press may suit small batches, sample production, or workshops that need flexible operation. A semi-automatic or automatic press may be more suitable when weight and output must stay consistent across many cycles.
The best option depends on the working pattern. Buying a more automated machine does not make sense if the production volume is low and the operator still needs to change molds often.
Suppliers may describe output as pieces per hour, but this number can change after installation.
The actual output depends on:
I prefer to calculate output from one complete cycle.
For example, if one cycle takes 20 seconds and produces one piece, the theoretical output is 180 pieces per hour. Actual output will be lower after filling, inspection, cleaning, and short stops are included.
If the mold produces four pieces per cycle, the calculation changes. Still, I need to confirm whether the four cavities can maintain similar weight and density. A higher cavity count may raise output while also increasing tooling cost and adjustment work.
A sample test can prevent an expensive mismatch.
I recommend sending the supplier enough powder for a practical trial. The test should record:
The test should not stop after one successful piece. A machine can make one acceptable sample and still show variation during continuous operation.
For a small ceramic parts workshop, a useful trial may involve several hundred pieces across multiple cycles. The team can then check weight variation, cracks, mold release, and cleaning time. This gives a better view of daily production than a single sample shown in a sales video.
A 50T powder press needs more than floor space.
I confirm:
Fine powder can enter moving parts and affect the working area. A suitable enclosure or dust control method may be needed, depending on the material.
The electrical details also matter. A machine designed for one voltage and frequency may require changes before it can be installed at another site. I ask for the wiring diagram and power requirements before arranging delivery.
A press with high force needs clear safety controls.
I look for:
The operator should not need to place hands near the mold during a normal cycle. Safe operation also depends on training, cleaning procedures, and routine inspection.
A low purchase price does not help if the machine requires unsafe workarounds.
The machine price is only one part of the budget.
I include:
A lower-priced machine may become more expensive if the mold is difficult to replace or spare parts take a long time to arrive. A higher-priced machine may be reasonable when it includes testing, documentation, training, and accessible technical support.
I ask for a written quotation with each item listed separately. This makes supplier comparisons more accurate.
A powder press is part of a production process, so service matters.
Before buying, I ask:
I also request photos or videos of the same model working with a similar material. A demonstration using a different powder may not show the conditions I will face.
Before I place an order, I make sure I can answer these questions:
A 50T rating can be a useful starting point, but it should not be the whole buying decision. I get better results when I compare the complete process: powder preparation, filling, pressing, ejection, inspection, cleaning, and maintenance.
The suitable machine is the one that matches the material, product, output plan, operator skill, and service conditions. A careful test and a detailed quotation can prevent many problems that are difficult to solve after delivery.

A 50T powder press can look like a simple production upgrade: apply up to 50 tons of force, form tablets, and keep output moving. My experience is that the rated force attracts most of the attention, while the costs around setup, tooling, powder handling, and maintenance decide whether the machine fits the operation.
A press with strong compression is not automatically the right press. The powder, tablet size, target weight, production rate, and quality checks all shape the buying decision.
The 50T rating usually refers to the maximum compression force the machine can apply. It does not tell me how well the press will perform with every powder or tablet design.
A useful evaluation includes:
A powder may need strong compression but still fail to form a stable tablet. Some blends cap, laminate, stick to the punch, or produce weight variation. A press can provide enough force while the feeding system struggles to deliver a consistent powder bed.
That is why I treat “50T” as a capacity reference, not a complete performance measure.
Higher compression force can support products that need stronger tablets or a more compact form. This may help with:
The actual result depends on dwell time, tooling, powder flow, moisture, lubricant level, and particle size. A machine running at a lower speed with stable feeding may produce better tablets than a faster machine operating near its force limit.
I also look at force distribution. A press should apply pressure in a controlled way across the tablet. Uneven pressure may create edge damage, cracks, or differences between tablets from different stations.
Tablet weight and thickness are not only cosmetic concerns. They affect packaging, dosing, dissolution, strength, and customer complaints.
When I assess precision, I ask how the machine controls:
A basic press may need frequent manual adjustment. That can work for small batches, but it adds labor and creates more room for variation. A system with force monitoring and controlled adjustment may reduce operator workload, though the purchase price and service needs may be higher.
For example, a supplement producer may run a calcium tablet in the morning and a smaller vitamin tablet later in the day. If the press has poor fill-depth control, the changeover may create a large number of tablets that need inspection or disposal. The machine may still be producing tablets, but the usable output is lower than the number shown on the production counter.
Tooling is one of the easiest costs to overlook.
A 50T press may require a specific punch and die standard. Tooling cost changes with:
A simple round tablet normally costs less to tool than a tablet with deep lettering, a curved profile, or a complex shape. Small design details can affect powder release and cleaning as well.
Tooling also wears over time. Damaged punches can create chipped tablets, sticking, and poor weight control. I recommend calculating tooling replacement as part of the operating cost instead of treating it as an occasional surprise.
The press cannot correct every powder problem.
Poor flow may cause inconsistent die filling. Excess moisture may lead to sticking. Too much lubricant may reduce tablet strength. A blend with different particle sizes may separate during transfer.
The surrounding process may need:
A buyer who focuses only on the press may discover that the real bottleneck sits before the press. If the powder arrives with unstable flow, higher press force will not solve the issue.
A 50T press needs more than floor space.
Before placing an order, I check:
A machine may fit through the workshop door but still be difficult to position, clean, or service. Poor access around the press can increase maintenance time and make routine inspections harder.
Dust control deserves close attention. Powder accumulation can affect sensors, moving parts, cleaning work, and workplace conditions. The required system depends on the material and local site rules.
A press can have a reasonable purchase price and still become expensive when small faults stop production.
Common downtime sources include:
I ask suppliers for a spare-parts list, recommended service intervals, response times, and training details. I also check whether technicians are available in my region.
A low-cost machine with limited technical support may create more risk than a higher-priced machine with accessible parts and clear service procedures. The right comparison uses total operating cost, not only the invoice value.
I use this process before approving a 50T powder press:
Define the product range
Record tablet diameter, weight, thickness, hardness, shape, and expected batch size.
Test the actual powder
Use the intended formulation or a close production sample. Check flow, moisture, sticking, capping, and ejection.
Confirm the working force
Ask for the normal operating range, not only the maximum rated force.
Review usable output
Compare theoretical speed with inspection results, rejected tablets, cleaning time, and changeover time.
Price the full setup
Include tooling, dust control, compressor capacity, dedusting, inspection equipment, installation, training, and spare parts.
Check cleaning and maintenance
Ask how long a standard changeover takes and which parts require regular replacement.
Request documentation
Review manuals, electrical drawings, maintenance schedules, material certificates, and test records.
A factory acceptance test using the buyer’s powder can reveal problems that a showroom demonstration will not show.
The main lesson I take from a 50T press is simple: force creates potential, while feeding, tooling, control, and maintenance create usable production. A careful buyer does not judge the machine by tonnage alone. I look at the complete process, calculate the costs that appear after installation, and confirm performance with the actual powder and tablet design.
Contact us today to learn more Hu: dgliheng168@163.com/WhatsApp +8613509684273.
Randall M German 1996 Sintering Theory and Practice
A W Jenike 1964 Storage and Flow of Solids
Dilip M Parikh 2016 Handbook of Pharmaceutical Granulation Technology
M J Cocks and W R Tiedeman 1998 Powder Compaction and Tableting
James S Reed 1995 Principles of Ceramics Processing
Randall M German 2005 Powder Metallurgy and Particulate Materials Processing
The 50T Press is designed to help manufacturers achieve up to three times faster production while lowering operating costs. By improving processing efficiency and reducing time per cycle, it enable
Tired of product defects and inconsistent results? Upgrade your production line with our powerful 50-ton hydraulic press, engineered to deliver stable pressure, precise forming, and dependable perf
50T powder molding technology provides the controlled force and stability needed to produce precise, reliable powder compacts for demanding manufacturing applications. By applying up to 50 tons of
Before buying a 50-ton press, take a closer look than the tonnage alone. The right machine should match your production needs, material requirements, tooling, and expected workload. Evaluate its tr
Email to this supplier

November 18, 2026

November 17, 2026
Contact

Send Inquiry
PRODUCT CATEGORIES
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.